Milk Begins Its Journey Before It Reaches the Factory
The production process starts at the dairy farm.
Raw milk must be collected, transported, received, tested, and stored under controlled conditions. At this stage, the factory needs reliable information about supplier, collection date, temperature, quantity, quality results, fat content, protein content, possible contaminants, and batch identification.
When the milk arrives, the ERP can connect receiving information with laboratory results, supplier records, purchase agreements, quality rules, and warehouse status.
If a batch does not meet the required standard, it can be placed into a controlled quality status rather than entering normal production automatically. If the batch is accepted, the system can link it to the production order and preserve its traceability throughout the rest of the process.
A dairy factory cannot control what it cannot trace.
Precision Processing Protects Quality
Dairy production depends on carefully controlled processing steps.
Depending on the product, milk may be separated, standardized, pasteurized, homogenized, fermented, cooled, mixed with additional ingredients, filled into containers, labelled, packed, and stored for delivery.
Each stage affects the final result.
Pasteurization is especially sensitive. The process must reach the correct time and temperature conditions to support food safety and product quality. Homogenization affects texture and prevents cream separation. Fermentation requires careful control for products such as yoghurt, cheese, sour cream, and other cultured dairy products.
Machines, sensors, Programmable Logic Controllers, known as PLCs, and SCADA systems can control these operational processes directly. SIX ERP can connect with the production environment to receive relevant data, record the production result, manage batch and quality information, and support planning and traceability.
It is important to understand the difference.
The factory control system manages the immediate machine action. The ERP provides the wider business context. It connects production with materials, orders, quality, warehouse stock, documents, costs, and management decisions.
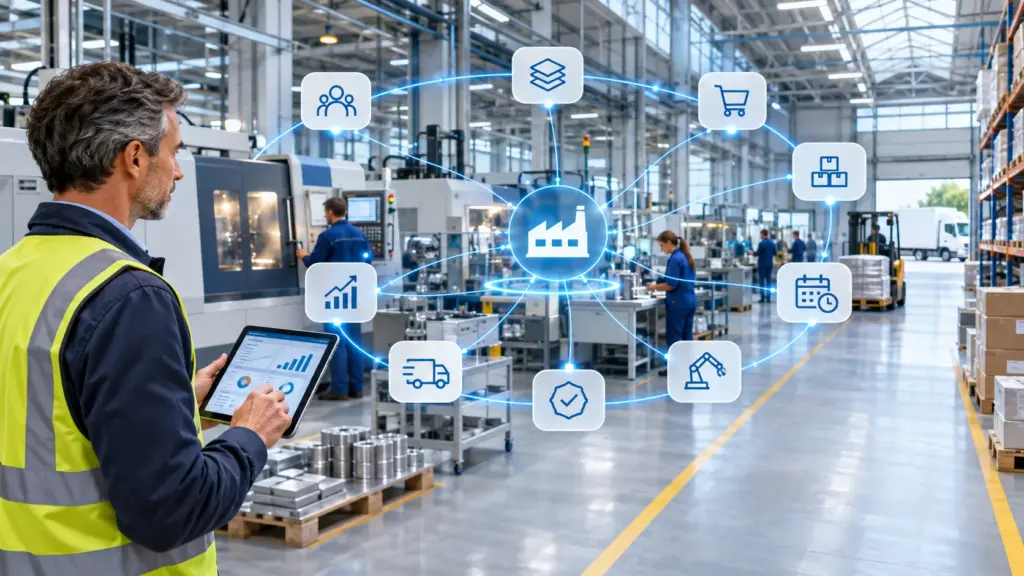
Together, these systems create a smarter production environment.
Real-Time Information Makes Problems Visible Earlier
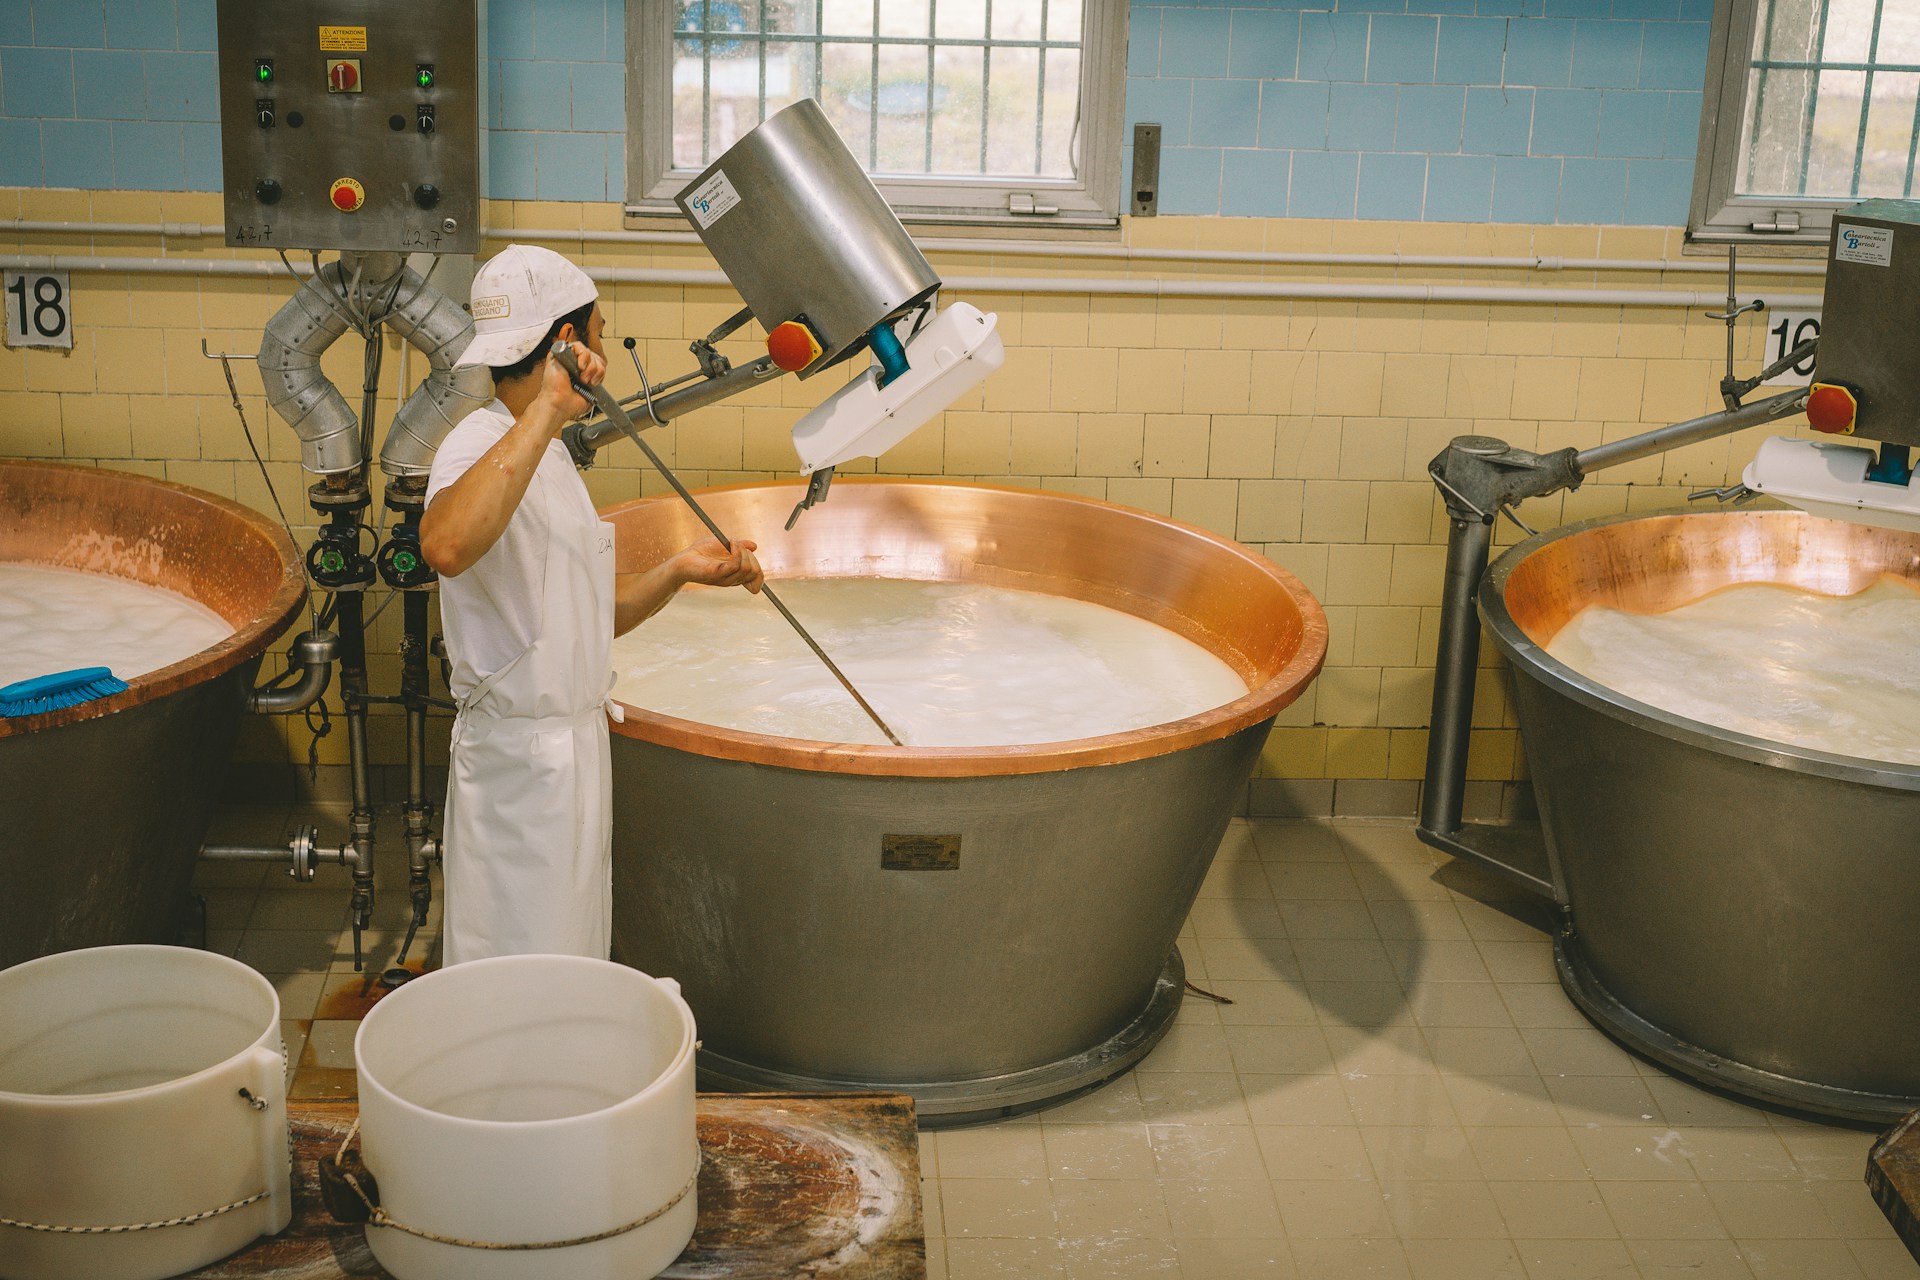
A modern dairy plant creates a large amount of information.
Temperature sensors can record storage and process conditions. Flow meters can measure liquid movement through pipelines. Scales can record ingredients and finished-product weights. Machine systems can report operating status, production speed, stoppages, and alarms. Laboratory systems can provide quality-test results.
When this information remains inside separate machines or local records, the company sees only part of the picture.
When relevant information is connected to the ERP, production managers can compare the plan with the actual result. They can see which batch was produced, which ingredients were used, how much material was consumed, whether there was waste, whether production was delayed, and where finished goods are stored.
This does not mean that every sensor alarm should create an automatic ERP decision. A reliable system needs clear rules.
For example, a serious deviation may require an immediate alarm for the production and quality team. A small deviation may require review and documentation. The ERP can record the event, link it to the batch, create a task, and help ensure the issue is investigated correctly.
Good information does not replace professional judgement. It helps the right people act faster.
Packaging Is Part of Quality Control, Food Safety, and Regulatory Compliance
In dairy manufacturing, packaging is much more than the final step before a product reaches the customer. It is an essential part of food safety, shelf-life protection, product identification, and regulatory compliance. Whether milk is filled into bottles, yogurt into cups, or cheese into sealed containers, the packaging must protect the product throughout storage, transportation, and distribution.
The European Union establishes specific requirements for packaging materials that come into contact with food. Under Regulation (EC) No 1935/2004, food-contact materials must not transfer substances into food at levels that could endanger human health or cause unacceptable changes to food composition or quality. The European Commission’s Food Contact Materials guidance also explains the importance of good manufacturing practices and the additional requirements that apply to certain packaging materials, including plastics.
Correct labeling is equally important. Regulation (EU) No 1169/2011 establishes requirements for food information provided to consumers. Depending on the product, mandatory information includes the product name, ingredients, allergens, net quantity, date marking, storage conditions, and nutritional information. For dairy manufacturers producing multiple varieties, fat contents, flavors, and packaging formats, using the correct approved label for each product is an essential quality-control requirement.
Batch identification adds another important layer of control. Under Directive 2011/91/EU, food products generally require identification of the production lot, subject to specified exceptions. The lot identification must be clearly visible, legible, and indelible. A date marking may serve as lot identification under the conditions defined in the directive. This enables manufacturers and authorities to identify products belonging to a particular manufacturing or packaging batch.
A connected ERP environment can support these obligations by linking finished-product batches with production orders, packaging material records, approved label versions, quality inspections, and customer deliveries. Through SIX ManufacturingFlow and SIX StockFlow, manufacturers can organize the operational information needed to track which materials were used, which products were manufactured, and where finished goods were distributed. Label verification, packaging approvalAn approval is a formal decision that allows a request or action to proceed. An ERP system can route approvals and record who made each decision., and batch-release controls must be defined and validated as part of the manufacturer’s actual quality process.
This becomes especially important when a packaging defect, incorrect allergen declaration, unsuitablSmart Dairy Manufacturinge food-contact material, or labeling error is discovered. Regulation (EC) No 178/2002, particularly Articles 18 and 19, establishes food traceability requirements and responsibilities concerning the withdrawal and recall of unsafe food. Properly maintained ERP records can help manufacturers identify affected product batches, determine which business customers received them, and provide information needed to support corrective actions and recalls.
For example, if a dairy manufacturer discovers that a packaging run used the wrong allergen label, the company should be able to investigate the affected production and packaging records, identify the relevant finished-product batches, and determine which deliveries may require attention. The actual response must follow an established food-safety assessment and withdrawal or recall procedure rather than relying on software alone.
Traceability is not paperwork completed after production. It must be built into every stage—from raw-milk receiving and processing to packaging, quality release, warehousing, and final delivery. When these activities are connected through reliable records and controlled procedures, dairy manufacturers are better equipped to protect consumers, respond to quality problems, and demonstrate compliance with applicable European food safety legislation.
Cold-Chain Control Continues Beyond the Factory
Milk and dairy products do not stop being sensitive once they leave the production line.
They must be stored, transported, and delivered under suitable conditions. The cold chain is part of product quality.
SIX ERP can connect production, warehouse, sales, and logistics information. It can show which finished-goods batches are available, where they are stored, which orders they are allocated to, and which deliveries are planned.
Where suitable technical solutions are available, temperature-monitoring devices and logistics platforms can provide additional transport and storage information. This can support faster action when a cold-chain problem occurs.
The ERP gives the company the wider business view: which customer orders are affected, which stock remains available, whether replacement production is needed, and how the issue should be documented.
Compliance Requires Reliable Records: Bulgarian Food Safety and Dairy Regulations
For dairy manufacturers operating in Bulgaria, regulatory compliance is not simply a matter of maintaining certificates or preparing documents for inspections. It requires continuous control over raw-milk quality, hygiene, production conditions, traceability, labeling, storage, and distribution. Every stage must generate reliable records that demonstrate how food safety is maintained.
The foundation is Bulgaria’s Food Act (Закон за храните), which regulates food production, processing, and distribution and establishes requirements for the registration or approval of food establishments. The Bulgarian Food Safety Agency (БАБХ) and its regional directorates are responsible for relevant official controls. Dairy manufacturers must operate within the applicable Bulgarian and European regulatory framework, including the specific requirements for establishments handling products of animal origin.
HACCP, Hygiene, and Dairy Production Controls
Under Regulation (EC) No 852/2004, food businesses must establish, implement, and maintain procedures based on Hazard Analysis and Critical Control Points (HACCP) principles. These procedures help manufacturers identify food safety hazards, establish necessary controls, monitor critical limits, document deviations, and implement corrective actions.
For dairy production, Regulation (EC) No 853/2004 introduces additional requirements for raw milk and dairy products. These include raw-milk hygiene and microbiological criteria, temperature management, handling conditions, and processing requirements. A Bulgarian dairy manufacturer therefore needs dependable records of incoming milk quantities, supplier identification, laboratory results, temperature checks, heat treatment, production batches, cleaning activities, and quality decisions.
ISO 22000 can provide an additional internationally recognized framework for food safety management. However, ISO 22000 certification is not generally a legal requirement for every Bulgarian dairy manufacturer. HACCP-based procedures and applicable food legislation are mandatory; certification may be required separately by customers, retailers, or contractual agreements.
Special Requirements Under Bulgarian Ordinance No. 26
Smaller dairy producers may also need to comply with Bulgarian Ordinance No. 26 of October 14, 2010 (Наредба № 26), which establishes specific rules for direct deliveries of small quantities of raw materials and foods of animal origin.
For operations falling within its scope, the ordinance addresses requirements such as raw-milk quality, laboratory testing, processing and storage conditions, product identification, documentation, and permitted distribution arrangements. It also includes specific requirements for certain small-scale milk-processing activities and associated records.
This distinction matters: Ordinance No. 26 is not a general substitute for the requirements governing every commercial dairy factory. Its applicability depends on the producer’s activities, production arrangements, quantities, and distribution model. Larger dairy-processing establishments must follow the general approval and hygiene requirements relevant to their operations.
Traceability, Quality Records, and Inspection Readiness
Under Regulation (EC) No 178/2002, food businesses must maintain traceability of relevant food materials and products. For Bulgarian dairy manufacturers, this means being able to identify where incoming materials originated and which business customers received finished products. Internal batch tracking strengthens this legal requirement by connecting the stages between receiving and distribution.
A properly configured ERP system can support these obligations by linking:
- Raw-milk receiving: supplier identification, collection dates, quantities, and incoming quality results.
- Production and processing: recipes, production orders, material consumption, processing parameters, and batch identification.
- Quality and hygiene: laboratory results, HACCP monitoring records, cleaning documentation, deviations, and corrective actions.
- Storage and distribution: warehouse movements, expiry dates, finished-product batches, and customer deliveries.
- Approvals and accountability: responsible employees, release decisions, document versions, and relevant audit records.
Through SIX ManufacturingFlow, SIX StockFlow, and SIX PurchaseFlow, dairy manufacturers can connect operational records that would otherwise be scattered across spreadsheets, paper documents, and separate systems. The specific quality-control, documentation, approval, and reporting workflows must be configured and validated against the manufacturer’s applicable requirements.
This becomes particularly valuable during inspections by the Bulgarian Food Safety Agency, internal food safety reviews, customer audits, or investigations into potentially unsafe products. Instead of reconstructing information from disconnected records, responsible employees can work from a consistent operational history.
Compliance becomes more reliable when accurate information is captured during normal production—not reconstructed when an inspector arrives. SIX ERP can provide the connected information foundation, while quality managers, laboratory specialists, and food safety professionals remain responsible for maintaining compliant procedures and verifying that they work.
Regulatory note: Bulgarian dairy requirements vary according to the establishment's approval status, production activities, products, and distribution model. The applicable obligations should be verified with the competent Bulgarian Food Safety Agency directorate and a qualified food safety specialist. ERP software supports compliance documentation but does not, by itself, establish regulatory compliance.
Sustainability Is Also an Efficiency Question
For dairy manufacturers, sustainability is closely connected to operational efficiency, resource management, and production costs. Every liter of milk, kilowatt-hour of electricity, cubic meter of water, and kilogram of packaging material represents an investment. When these resources are consumed unnecessarily, the factory loses money while increasing its environmental impact.
Dairy processing is particularly resource-intensive. Pasteurization, cooling, refrigeration, fermentation, cleaning-in-place (CIP) systems, and packaging equipment all require energy, water, and other resources. Poor production scheduling, excessive cleaning cycles, equipment inefficiencies, rejected batches, inaccurate recipes, and expired finished products can increase consumption without generating additional value.
The European Commission’s Joint Research Centre addresses these challenges in its Best Environmental Management Practices for the Food and Beverage Manufacturing Sector. Its recommendations include optimizing cleaning procedures, reducing unnecessary water and chemical consumption, improving production scheduling, and monitoring resource efficiency.
Connecting Sustainability with Everyday Dairy Production
Sustainability improvements become more practical when manufacturers can measure where resources are consumed and where losses occur.
SIX ManufacturingFlow connects production orders, material requirements, actual consumption, manufacturing output, and recorded waste. This allows production managers to compare planned and actual material usage, investigate yield differences, and identify products or production stages where losses repeatedly occur.
Meanwhile, SIX StockFlow supports inventory visibility, batch tracking, and stock movements. For dairy manufacturers, accurate inventory management is essential because raw milk, ingredients, intermediate products, and finished dairy goods often have limited shelf lives. Better stock visibility helps teams identify products approaching expiry, avoid unnecessary purchasing, and coordinate production with available materials.
Financial information adds another dimension. By connecting production records with SIX FinanceFlow, manufacturers can examine the costs associated with material consumption, production losses, packaging, and other operational expenses. Energy and water consumption can also contribute to this analysis when reliable measurements are collected and integrated from meters, equipment, or other systems.
The objective is to understand not only how much the factory produces, but how efficiently it converts resources into saleable products.
Reducing Food Waste Through Better Planning and Traceability
Food waste is both an environmental problem and a financial burden. In dairy manufacturing, losses can occur during milk receiving, processing, product changeovers, packaging, storage, and distribution. Some waste results from unavoidable processing conditions, while other losses arise from poor planning, handling mistakes, quality failures, or excess production.
The European Union has made food waste reduction a policy priority. Under the revised EU Waste Framework Directive (EU) 2025/1892, Member States must take measures to reduce food waste generated in processing and manufacturing by 10% by 2030, compared with the average for 2021–2023. This is a national-level reduction target, not an identical mandatory reduction quota imposed on every individual dairy factory.
The European Commission’s food waste measurement framework emphasizes consistent measurement as the foundation for effective prevention. For dairy manufacturers, that means distinguishing between processing losses, rejected materials, waste from expired products, and usable by-products rather than combining every difference into one general waste figure.
Accurate batch information, production records, inventory movements, and quality results help managers investigate these losses and determine which corrective actions are appropriate. Our article on Supply Chain Resilience also explains why reliable stock information and better preparation for supply disruptions matter to manufacturing continuity.
From Sustainability Reporting to Better Decisions
Once resource consumption and production losses become measurable, management can investigate the questions that matter most:
- Which dairy products generate the highest material losses or waste?
- Which production lines have the largest differences between planned and actual consumption?
- Are ingredients, packaging materials, or finished products being discarded unnecessarily?
- Can production schedules reduce changeovers and unnecessary cleaning cycles without compromising food safety?
- Are products approaching expiry because production quantities exceed actual demand?
- Which processes consume the most energy and water per kilogram or liter of finished product?
The answers can support practical improvements in scheduling, purchasing, inventory control, equipment maintenance, and cost management.
However, an ERP system cannot measure every environmental indicator automatically. Reliable energy, water, and emissions reporting may require additional metering, equipment integrations, and appropriate calculation methods. Similarly, environmental performance should be assessed alongside food safety, product quality, and hygiene requirements—not at their expense.
Sustainability becomes practical when it is measured, managed, and connected to everyday production decisions. For dairy manufacturers, reducing unnecessary consumption and waste is not only an environmental responsibility. It is also an opportunity to improve operating costs, protect product quality, and build a more efficient and resilient business.
Building the Digital Model Before Go-Live
A successful dairy ERP implementation begins long before the first production order is processed. At SIX ERP, the starting point is a detailed analysis of the factory’s existing processes, operational dependencies, and information flows. The objective is to build a reliable digital model of how the business actually works before introducing automationAutomation uses software or equipment to carry out tasks according to defined rules. An ERP system can automate routine business steps and highlight exceptions for review..
The project team maps the complete dairy production cycle, from raw-milk receiving and quality inspection to storage, recipes, bills of materials (BOMs), processing, packaging, finished-goods handling, and distribution. Each stage must connect with purchasing, warehouse operations, production planning, quality control, and financial reporting. As explained in our article on ERP Selection and Migration, understanding existing processes and identifying operational gaps is essential before designing the future ERP environment.
Particular attention must be given to product master data, measurement units, batch identification, recipes, material consumption, and traceability. Dairy manufacturers frequently work with kilograms, liters, individual packages, and production batches, making accurate data relationships critical. Our guide to ERP System Data explains why consistent records, validated material definitions, and reliable data structures are necessary before automation can deliver dependable results.
Once these processes are documented, the team can evaluate realistic operating scenarios. What happens when an incoming milk delivery fails quality inspection? How should production react when a required ingredient is unavailable? Can a finished batch be blocked from sale until quality approval is completed? What happens when packaging materials arrive late or an urgent customer order changes production priorities?
These scenarios are especially important because dairy manufacturing depends on coordinated production schedules, short processing windows, material availability, and strict quality requirements. Our article on Supply Chain Resilience explains how testing supplier disruptions, material shortages, and alternative sourcing decisions can reveal operational weaknesses before they affect production.
The resulting digital model becomes the foundation for the SIX ERP Business Blueprint. It defines how information should move between departments, which processes require approval, where traceability must be maintained, and how exceptions should be handled. The implementation can then be organized into manageable stages, with realistic test cases, employee training, and clearly defined responsibilities. Our guide to ERP Systems and Successful Implementation explains why process mappingProcess mapping documents the steps, people and decisions involved in business work. In an ERP project, it helps define workflows and identify improvements before system setup., clean data, phased deployment, and practical employee training are essential for a reliable go-live.
The objective is not simply to digitize existing factory procedures. It is to create a connected, tested, and manageable production environment before daily operations depend on it. Careful preparation cannot eliminate every future disruption, but it helps dairy manufacturers identify weaknesses earlier, reduce implementation risks, and establish a stronger foundation for continuous improvement.
Integration With Machines Must Be Designed Carefully
Dairy factories often use PLCs, SCADA systems, laboratory systems, industrial scales, sensors, temperature monitors, barcode equipment, and specialized production machinery.
Connecting these systems to ERP requires careful planning.
The business must decide which data should move into the ERP, how often it should update, who owns the data, and what should happen if information is missing or incorrect. It should not try to transfer every possible machine value without a clear reason.
For example, the ERP may need production quantities, batch numbers, material consumption, machine downtime summaries, quality statuses, and confirmed process results. The SCADA system may keep detailed second-by-second machine-control data. Each system should do the job it is designed to do.
A good integrationIntegration connects systems so they can exchange information or coordinate actions. An ERP integration helps link business tools and reduce manual transfers between them. makes the factory clearer. A poorly designed integration creates another source of confusion.
People Make the Smart Factory Work
Technology alone does not make a dairy factory more efficient. Successful digital transformation depends on the people who understand the production process, manage daily operations, and make decisions. SIX ERP connects these employees through specialized solutions that allow every department to work with the same reliable information.
Production operators and managers use SIX ManufacturingFlow to coordinate production orders, monitor machines, record material consumption, and manage quality checks throughout dairy processing. Quality teams can follow production batches, inspect results, and maintain traceability from raw milk to finished dairy products.
Warehouse employees rely on SIX StockFlow to manage raw materials, packaging, storage locations, batch numbers, expiry dates, and inventory movements. Purchasing teams use SIX PurchaseFlow to coordinate suppliers, manage purchasing requirements, and ensure that materials arrive when production needs them.
Meanwhile, SIX FinanceFlow connects operational transactions with financial information, helping finance teams understand production costs, purchasing expenses, waste, and profitability. SIX PeopleFlow supports workforce management by organizing employee availability, working hours, qualifications, and competencies, helping managers assign appropriately trained employees to production activities.
A successful SIX ERP implementation involves these teams from the beginning. Their practical experience helps identify inefficient processes, define realistic workflows, and ensure that the system reflects how the dairy factory actually operates. Involving employees early also encourages acceptance of new procedures and makes the transition easier.
The goal is not to replace experienced employees with software. It is to connect their knowledge, responsibilities, and daily activities through one integrated systemAn integrated system connects business functions or applications so they can share information. An ERP system uses this approach to link operations and reduce repeated data entry.. When production, quality, purchasing, warehouse, HR, and finance teams work together, the dairy factory gains better operational control, clearer accountability, and more time to focus on product quality, food safety, and continuous improvement.
The Result: A More Responsive, Compliant, and Future-Ready Dairy Business
A connected ERP environment gives dairy manufacturers much more than an overview of production orders. It creates a reliable information flow connecting raw-milk deliveries, quality inspections, production batches, recipes, packaging, warehouse inventory, customer orders, distribution, and financial performance. Instead of managing these activities separately, the company gains a real-time view of its entire operation and can identify problems before they affect production or customer deliveries.
For European dairy producers, this visibility is particularly important because operational efficiency must go hand in hand with food safety and regulatory compliance. The European Commission’s General Food Law framework, established under Regulation (EC) No 178/2002, requires food businesses to maintain traceability throughout the food chain. A properly configured ERP system can support these obligations by connecting incoming raw-milk batches with production records, finished products, and outgoing deliveries. This information helps manufacturers investigate quality issues, identify affected batches, and organize product withdrawals or recalls when necessary.
Quality management is equally important. The European Commission’s food hygiene legislation, including Regulations (EC) No 852/2004 and No 853/2004, establishes hygiene requirements for food businesses, with additional specific provisions for products of animal origin. Dairy manufacturers must manage hygiene, temperature controls, production conditions, and food safety procedures appropriate to their operations. Connecting inspection results, production activities, and batch records within ERP helps employees maintain the documentation and operational oversight needed to support these responsibilities.
A connected system also helps manufacturers reduce unnecessary losses. By monitoring raw-material consumption, production yields, rejected batches, expiry dates, and finished-goods inventory, companies can identify where materials are wasted and where processes need improvement. These efforts align with the European Commission’s initiatives to reduce food waste, which promote better measurement, prevention, and management of food waste across the European food supply chain.
As dairy manufacturers expand, their operational requirements become more complex. New yogurt and cheese varieties introduce additional recipes, ingredients, processing stages, and quality specifications. New packaging formats require different materials and labeling information, while additional warehouses and distribution channels introduce further inventory and traceability requirements. The EU Food Information to Consumers Regulation (EU) No 1169/2011 establishes requirements for food labeling, including ingredients, allergens, and nutritional information. Reliable product and ingredient data helps manufacturers prepare and maintain accurate labels as their product portfolios grow.
With SIX ERP connecting manufacturing, purchasing, warehouse operations, quality-related processes, sales, and finance, dairy producers can build a structured operational foundation that supports both daily production and future expansion. Regulatory compliance still depends on correctly designed processes, validated records, appropriate controls, and responsible employees. Software supports these requirements but does not replace them.
The result is a dairy factory that is not only automated, but informed, traceable, adaptable, and better prepared for growth. Management can make decisions using current operational information, employees can respond more quickly to disruptions, and the business can improve production efficiency while maintaining the quality and food safety standards its customers expect.
Build Your Dairy Operation for the Future
Every dairy manufacturer faces different challenges.
You may need stronger batch traceability, better production planning, controlled recipe management, tighter warehouse processes, clearer quality records, less waste, more reliable cold-chain visibility, or better management reporting.
SIX ERP helps dairy and food manufacturers connect these processes into one practical business system.
Talk to the SIX ERP team about your dairy production process. Together, we can build the data flow, traceability, planning, and operational control needed to protect quality today and support growth tomorrow.