Tips and Tricks for Manufacturing companies for a successful EPR implementation
“The key is not to prioritise what is on your schedule. It is to schedule your priorities.”
A manufacturing company cannot grow on guesswork.
When sales orders, raw materials, production plans, warehouse stock, machines, quality checks, deliveries, and invoices are managed in separate files, the business starts losing time long before anyone notices. Employees ask each other for updates. Production waits for missing materials. Sales promises delivery dates without seeing real capacity. Managers receive reports after the problem has already happened.
This is where a manufacturing ERPAn ERP system connects a company’s core processes—such as sales, finance, inventory, manufacturing, and service—in one place so teams can work with shared information. system makes the difference.
ERP is not just software for invoices or inventory. It is the connected operational backbone of the factory. It brings information from the customer order to the production floor, warehouse, delivery, invoice, and final business result into one controlled process.
If your manufacturing business is growing, struggling with Excel files, facing stock uncertainty, or spending too much time chasing information, now is the time to look at ERP seriously.
What ERP Changes Inside a Manufacturing Business
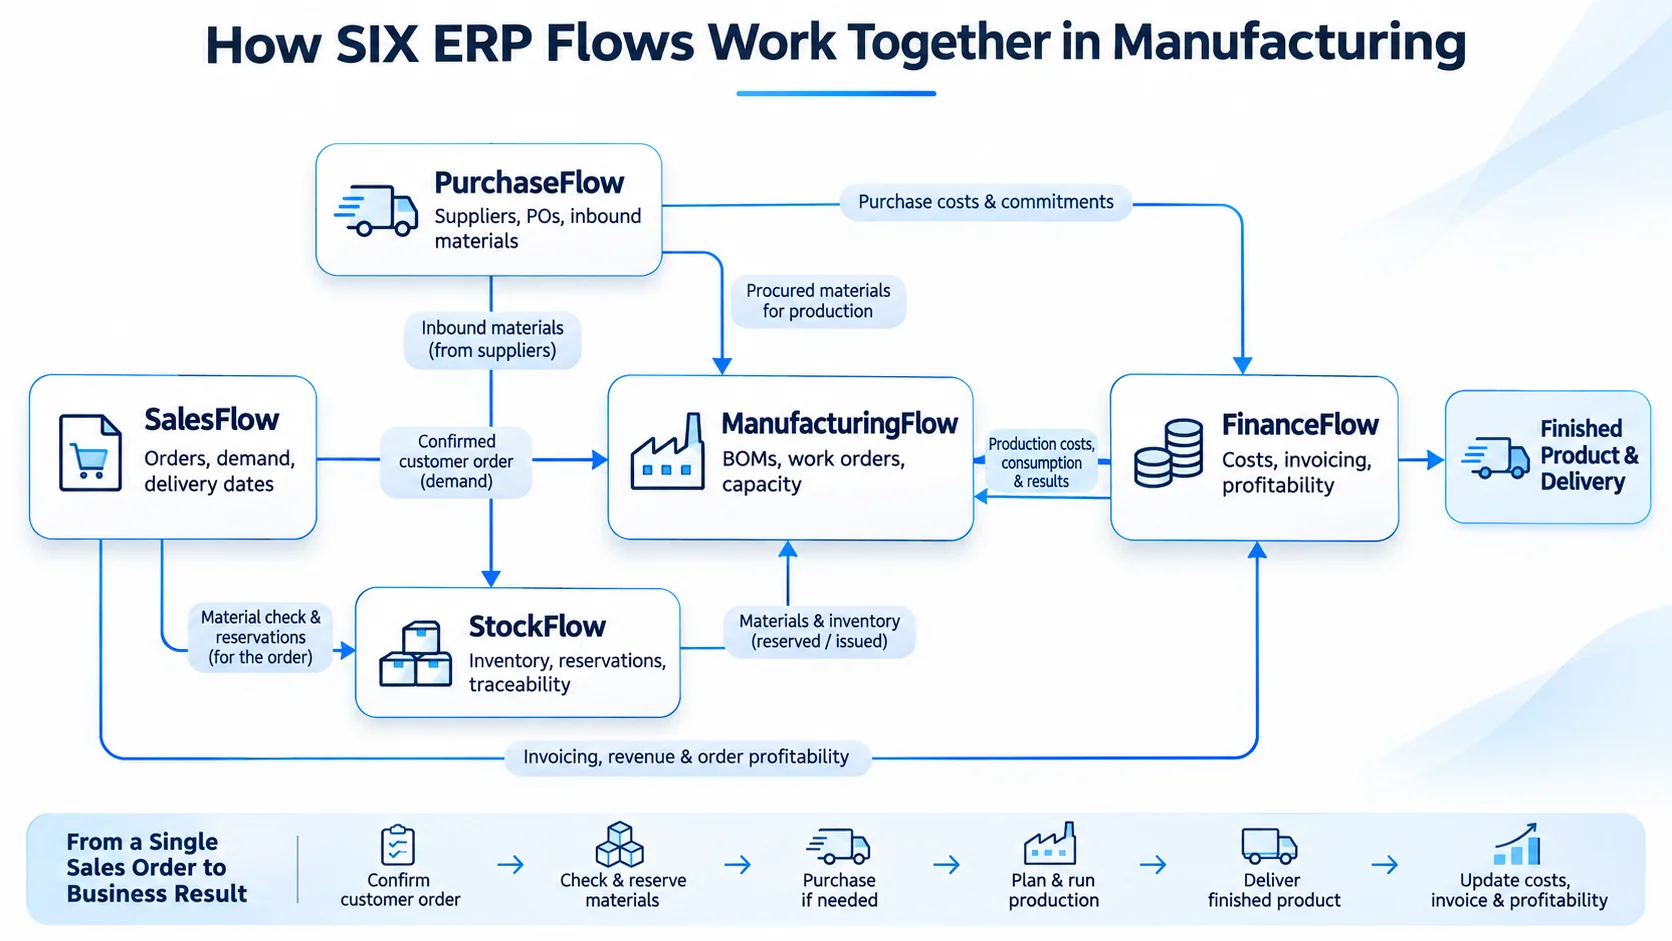
SIX ManufacturingFlow connects manufacturing operations with the departments that must work together to turn customer demand into finished products. Instead of managing sales, purchasing, inventory, production, and finance separately, SIX ERP brings these activities into one integrated systemAn integrated system connects business functions or applications so they can share information. An ERP system uses this approach to link operations and reduce repeated data entry. where information flows between teams in real time.
With SIX SalesFlow, sales teams can check product availability, manage customer orders, and identify when production is required. SIX PurchaseFlow helps purchasing teams identify material requirements, coordinate suppliers, and monitor incoming deliveries. SIX StockFlow connects warehouse operations with purchasing and production, providing accurate information about available materials, stock reservations, warehouse movements, and traceabilityTraceability follows a product or material through its history, from origin to use or delivery. An ERP system connects the records needed to investigate issues and track affected items..
At the center of the factory, SIX ManufacturingFlow connects bills of materials (BOMs), production orders, work centers, machines, employees, and manufacturing schedules. Production managers can monitor progress, identify bottlenecks, and respond to material shortages or capacity constraints. Meanwhile, SIX FinanceFlow connects operational transactions with financial records, helping management understand material costs, labor expenses, manufacturing costs, and product profitability.
These connected SIX Flows eliminate the need for departments to maintain separate versions of the same information. A confirmed customer order can generate manufacturing demand, trigger material availability checks, reserve existing stock, and identify additional purchasing requirements. Production can then be scheduled according to available resources, while completed manufacturing orders update inventory and support delivery, invoicing, and cost calculations.
The result is one connected manufacturing process, from the first customer order to the finished product and its financial outcome. Management gains a real-time view of operations, helping teams make informed decisions, prevent avoidable delays, and keep production moving efficiently.
Choose an ERP That Understands Manufacturing
Not every ERP system is designed for the realities of manufacturing.
A manufacturer needs more than customer records and invoices. The system must support bills of materials, product structures, raw materials, work orders, work centers, routings, warehouse locations, production scheduling, material consumption, finished goods, waste, quality checks, and traceability.
For some businesses, it must also support serial numbers, batches, expiry dates, subcontractors, multiple warehouses, different units of measure, customer-specific products, technical documents, or machine connections.
The right ERP should match the way your factory works today while giving you a better structure for tomorrow.
It must also be practical for the people using it. Warehouse employees need clear stock and scanning functions. Production users need simple work orders and reporting tools. Sales teams need accurate product, availability, and delivery information. Management needs reports that show what is happening without waiting for someone to combine several Excel files.
Start With the Real Factory Process
A successful manufacturing ERP implementation begins long before the software is installed. It starts with understanding how the factory actually operates, identifying weaknesses, and defining how people, processes, and information should work together.
Every manufacturer has its own operational requirements. How does a customer inquiry become a confirmed sales order? How are production orders planned and scheduled? When are raw materials purchased, received, and reserved? How do materials move through the warehouse and onto the production floor? How are quality checks, finished goods, deliveries, and invoices managed?
Answering these questions requires more than a software demonstration. Through SIX ERP Consulting, our consultants work with management and operational teams to examine existing processes, identify dependencies, and establish clear business requirements before implementation begins.
This analysis often reveals problems that have become part of everyday operations. Inventory records may not match physical stock. Bills of Materials (BOMs) may contain outdated specifications. Production planning may depend on individual spreadsheets, while purchasing and finance work with different information. These weaknesses can create delays, unnecessary costs, and unreliable management reporting.
To address these challenges systematically, SIX follows its 7-Step Consultation Flow, a structured approach that moves from understanding the business to preparing and delivering operational improvements. The process establishes business direction, maps existing workflows, identifies gaps, designs improved processes, prepares the organization, plans implementation, and supports adoption.
The findings form the basis of a Business Blueprint, defining the required ERP processes, priorities, responsibilities, integrations, and implementation stages. This helps manufacturers understand what needs to change, why it matters, and how the transition should be organized.
The objective is not to force a factory to adapt to software. It is to understand the business, improve inefficient processes, and configure SIX ERP around a clear, practical operating model. A well-prepared Business Blueprint reduces uncertainty, supports realistic implementation planning, and establishes the foundation for long-term operational improvement.
Warehouse and Inventory Control Are Essential
Manufacturing depends on having the right materials in the right place at the right time.
If stock information is incorrect, production stops. If too much material is purchased, money is trapped in the warehouse. If materials are not traceable, quality issues become difficult to investigate. If finished goods cannot be located quickly, deliveries are delayed.
A manufacturing ERP must connect the warehouse directly to purchasing, production, and sales.
It should show what is physically available, what is reserved, what is expected from suppliers, what is issued to production, what is in progress, and what is ready for delivery. It should also support batch numbers, serial numbers, warehouse locations, stock transfers, stock counts, returns, and quality-related status where required.
When inventory is accurate, the entire factory becomes more reliable.
Production Planning Should Be Based on Facts
Production planning is difficult when it depends only on experience, phone calls, and informal messages.
A production manager needs to see customer demand, deadlines, available materials, machine capacity, employee availability, open work orders, and possible delays. Without this information, planning becomes a daily emergency exercise.
ERP helps create a more controlled schedule.
The system can show what needs to be produced, what materials are required, whether these materials are available, and where capacity may be limited. If a supplier is late, the business can see which production orders and customer deliveries may be affected. If demand changes, planners can review the impact before making promises.
This does not remove the need for experienced production managers. It gives them better information to make better decisions.
Training Turns ERP Into a Working System
A manufacturing ERP is only valuable when people use it correctly.
Employees need to understand their own part of the process. Warehouse teams need practical training on receiving, locations, stock movements, picking, and material issue. Production users need to understand work orders, material consumption, reporting, and quality steps. Sales teams need to see how their orders affect stock, planning, and delivery. Managers need to know how to use reports and dashboards.
Training should be based on real factory situations, not only generic software demonstrations.
At SIX ERP, implementation includes practical training and change support. The aim is not to leave employees with a login and a manual. The aim is to help them feel confident using the system in their normal work.
Avoid the Most Common ERP Mistakes
The biggest mistake is trying to change everything at once.
A manufacturing ERP project should have a clear direction, but it should also be divided into manageable phases. Core processes such as products, customers, purchasing, warehouse, production orders, and invoicing should work reliably before the company adds more advanced automationAutomation uses software or equipment to carry out tasks according to defined rules. An ERP system can automate routine business steps and highlight exceptions for review., specialist integrations, or complex reporting.
Another common mistake is importing poor data into a new system. Old product records, duplicate suppliers, incorrect units of measure, outdated prices, and unreliable stock data should be reviewed before migration. A new ERP should not become a cleaner-looking home for old problems.
A third mistake is treating ERP as an IT project. It is a business project. Production, warehouse, purchasing, finance, sales, and management all need to be involved. The people who perform the work every day understand details that no software demonstration can reveal.
Use ERP to Improve Every Day
ERP should not become a system that is only used to record what has already happened.
It should help the company improve continuously.
Management can monitor production delays, material shortages, waste levels, supplier performance, stock turnover, delivery reliability, product costs, sales margins, and customer demand. When a problem appears, the business can investigate earlier and act before it becomes expensive.
For example, if scrap increases for one product, production and quality teams can review the process. If a supplier repeatedly delivers late, purchasing can address the issue. If a finished product is less profitable than expected, management can review material costs, labor time, waste, and selling price.
This is the real value of ERP: it turns daily activity into information that supports better action.
Your Factory Does Not Need More Spreadsheets
Your factory needs a connected process.
SIX ERP brings sales, purchasing, warehouse management, production, finance, HR, quality-related workflows, and Business Intelligence together in one flexible system. It gives your team the information needed to plan production, control materials, meet delivery promises, understand costs, and grow with confidence.
Whether you are starting your ERP journey or replacing a system that no longer fits the way your factory works, our team can help you assess your process and build the right implementation plan.
Book a SIX ERP manufacturing consultation today. Let us look at your production flow, warehouse process, data challenges, and growth plans — and show you how a connected ERP can move your factory from daily firefighting to real operational control.